Professional EMC Filters for Reliable Electronic Design
2026-10-18
Reliable electronic design doesn't leave electromagnetic compatibility to chance. Yet many teams still treat EMC filters as a late-stage checkbox rather than a core design element. DOREXS takes a different approach—building professional filters that keep noise out and performance stable. If you've ever wondered why some boards pass emissions tests while others fail mysteriously, the answer usually starts here.
Why EMC Filters Decide Whether Your Design Survives the Real World
Every circuit board looks flawless on the bench, but the moment it leaves the lab, it enters a battlefield of electromagnetic noise. Motors, radio transmitters, switching power supplies, even nearby mobile phones can inject interference that corrupts signals or resets microcontrollers. An EMC filter is not just another passive component—it is the difference between a product that works only in isolation and one that keeps functioning when a forklift drives past or a relay switches nearby.
Many designers treat EMC as a final checkbox, bolting on a filter after a failed compliance test. That approach almost always backfires. Filter placement, grounding, component parasitics, and board layout determine whether the filter actually suppresses the frequencies causing trouble. A poorly chosen filter can even create new resonance peaks, making emissions worse. The products that survive real-world conditions are those where the filter is considered from the first schematic sketch, not as an afterthought.
The real world also punishes overdesign. Oversized filters consume board space, add cost, and can degrade signal integrity by attenuating legitimate high-speed edges. The goal is not to eliminate all noise—that is impossible—but to control it precisely where it threatens functionality or exceeds legal limits. Get that balance right, and the design works not just in the test chamber but for years in the field, under voltage spikes, temperature swings, and constant electromagnetic chaos.
The Hidden Costs of Skimping on Filter Performance
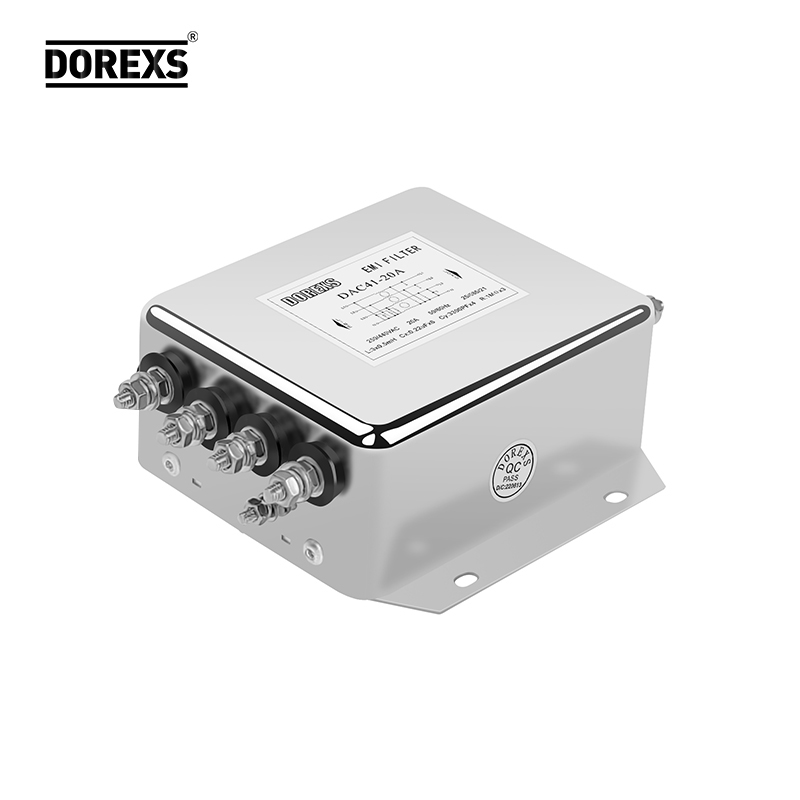
When a filter is specified down to the cheapest possible option, the immediate savings are easy to see on a purchase order. What doesn't show up there is the real cost of pushing a system harder to compensate for poor filtration. Pumps run longer, pressure drops climb, and energy bills quietly rise month after month. In many facilities, the extra electricity consumed by a struggling filter loop exceeds the money saved on the filter itself within the first year.
There is also the wear-and-tear factor that few budget sheets capture. Contaminants that slip through a low-performance filter end up scoring cylinder walls, clogging precision valves, and accelerating oil degradation. Each of those failures leads to unscheduled downtime, which is usually far more expensive than the filter element that could have prevented it. Maintenance teams learn to dread the "bargain" filter because it simply shifts the workload from procurement to the repair bay.
Finally, the hidden costs extend to product quality and reputation. In food processing, pharmaceuticals, or paint finishing, a poorly performing filter can introduce defects that are only caught after batches are complete. Rework, scrap, and even customer returns become part of the equation. Once those numbers are added up, the so-called cheap filter often turns out to be the most expensive component in the entire line.
Matching Filter Topology to Signal Integrity Goals
Choosing the right filter arrangement starts with the specific demands of your signal path. A low-pass topology, for instance, suppresses unwanted high-frequency harmonics without disrupting the fundamental waveform, while a band-pass design isolates a narrow frequency range when adjacent channels or noise sources threaten the eye diagram. The physical layout of the filter also matters more than many engineers assume: a T-network offers better input-to-output isolation than a simple L-section, but it consumes more board space and can introduce additional parasitic capacitance.
Signal integrity is not only about attenuation—reflection and group delay often decide whether a filter helps or hurts. A sharp roll-off might clean the spectrum yet cause ringing on fast edges due to phase distortion near the cutoff. In high-speed differential links, symmetric filter placement preserves common-mode rejection, whereas an asymmetric layout can convert common-mode noise into differential errors. Matching the topology to the signal's rise time, voltage swing, and bandwidth requirement prevents the filter from becoming a new source of jitter.
Practical pairing guidelines begin with the PCB stackup and termination impedance. For example, a capacitor-to-ground at the receiver works well when source impedance is low, but the same element placed at a high-impedance node creates reflections. Mixed topologies—such as a series ferrite bead followed by a shunt capacitor—offer wideband suppression, yet their interaction with trace parasitics must be verified through time-domain reflectometry or eye-pattern measurements rather than relying on ideal SPICE models.
Thermal and Layout Pitfalls That Undermine Filter Ratings
The numbers on a filter datasheet are usually taken on a bench at room temperature, with the device sitting by itself. Put that same filter next to a linear regulator or a high-current DC-DC converter, and the operating temperature climbs. Ferrite cores in common-mode chokes lose permeability as they heat up, so the impedance meant to block noise drops. Ceramic capacitors with X7R or X5R dielectrics can drift significantly at elevated temperatures, shifting the resonant point and leaving a hole in the attenuation curve where you least expect it.
Layout can be just as unforgiving. If the input and output traces run parallel for a few millimeters, high-frequency noise hops across the tiny parasitic capacitance between them, completely bypassing the filter components. Vias that carry return current may look fine on the schematic but add nanohenries of inductance that chew into the high-end insertion loss. Inner-layer splits or gaps in the ground plane under the filter create a slot antenna effect, feeding noise from the dirty side to the clean side without ever touching the inductor or capacitors.
The combined impact is that a filter rated for 40 dB of attenuation at 100 MHz might deliver only 25 dB once thermal and layout realities set in. Rather than trusting the datasheet curve, it pays to re-measure the board under full load and with the enclosure closed. Keep the ground path from filter capacitors to the return plane as short as possible, pour copper directly beneath the filter to spread heat, and never route input and output traces side by side. These steps help the printed rating survive contact with a real board.
Testing Beyond the Datasheet: What Actually Happens in the Field
Datasheets promise clean supply rails, tame loads, and room-temperature benches. Real installations laugh at those assumptions. A motor drive tucked next to a welding bay sees line transients that make the spec sheet's worst-case ripple look like a polite suggestion. Thermal derating curves assume still air, yet most enclosures breathe through filters clogged with shop dust within a month. Engineers who trust the printed limits without probing actual field behavior end up chasing intermittent faults that never reproduce on the bench.
Field failures rarely stem from a component exceeding its absolute maximum rating in a tidy, predictable way. Instead, they creep in through edge cases: inrush currents during cold starts, ground bounce when a nearby relay drops out, or noise coupling from a cable routed too close to a VFD output. One power supply we examined passed every datasheet test with margin, yet failed within weeks in a solar installation. The culprit? Morning dew condensing on the PCB, creating a leakage path that shifted the feedback divider just enough to push the output out of regulation. No datasheet paragraph covers that.
The real lesson is to treat datasheets as a starting point, not a verdict. Test with the actual load, in the actual enclosure, with the actual wiring harness. Add deliberate abuse: hot plugging, brownouts, load steps that occur while the input capacitor is still charging. Instrument what the datasheet doesn't show—transient voltage at the switch node, temperature gradients across the board, ringing on the ground plane. That's where the field writes its own spec, and it rarely matches the marketing department's version.
Designing for Compliance Without Over-Engineering the BOM
Striking the right balance between regulatory compliance and a lean bill of materials often feels like threading a needle. Many teams default to adding redundant components or over-specifying parts just to feel safe, but that approach quietly bloats cost, lead time, and assembly complexity. The real goal is to understand which compliance requirements actually drive BOM structure, and which ones can be satisfied through documentation, testing, or process controls instead of physical parts. When you treat compliance as an information problem as much as a hardware problem, you stop bolting on unnecessary safeguards.
One practical lever is to lean on pre-certified modules and off-the-shelf components that already carry the needed ratings—UL, CE, RoHS, or whatever applies. Rather than designing a custom power supply from scratch and then proving its safety, you drop in a certified brick and reference its certificate in your technical file. This keeps the BOM short while still passing audits, because the compliance evidence lives in the supplier documentation, not in extra hardware. Similarly, consolidating functions into fewer, smarter ICs or using a single connector family across multiple compliance zones can remove entire line items without weakening the design.
Avoiding over-engineering also means challenging every 'just in case' part during design reviews. If a ferrite bead, a secondary fuse, or a redundant voltage monitor is added solely because someone worried about a vague regulatory risk, it's probably a candidate for removal. Instead, map each BOM line to a specific standard clause or a tested failure mode. When you can't point to a clear requirement, you've found over-engineering. This disciplined mapping not only trims the BOM but also makes future compliance updates simpler, since each remaining component has a known, justified purpose.
FAQ
Without proper filtering, high-frequency noise from power lines or signal cables can couple into sensitive circuits, causing erratic behavior, data corruption, or even permanent damage. Professional EMC filters use carefully selected components and shielding to suppress both common-mode and differential-mode interference before it reaches critical stages, which keeps the system stable across real-world operating conditions.
Start with the maximum continuous current your device draws, then add a margin for inrush and transient peaks. Running a filter too close to its rated current raises internal temperature, which degrades capacitors and inductors over time and reduces filtering performance. A common practice is to derate by at least 20-30% for sustained loads, especially in enclosed or high-ambient-temperature installations.
Differential-mode noise flows between line and neutral (or positive and return) and is usually caused by switching currents. Common-mode noise appears on both conductors relative to earth ground, often from capacitive coupling or unbalanced impedances. Professional filters combine X capacitors and chokes for differential-mode suppression with Y capacitors and common-mode chokes for common-mode suppression, so both paths are handled in one package.
Not entirely. A filter primarily targets conducted emissions below about 30 MHz by attenuating noise traveling along cables and PCB traces. Radiated emissions typically require shielding, proper grounding, and careful layout as well. However, a well-designed filter can reduce the source energy that would otherwise radiate from cables acting as antennas, so it indirectly helps with radiated problems too.
Long input or output leads, poor grounding, and routing filtered and unfiltered wiring together are the biggest culprits. If the filter's ground connection is weak or inductive, common-mode currents bypass the filter and re-enter the system. Also, mounting the filter far from the equipment entry point allows noise to couple back onto the cables after filtering. Keep leads short, use a low-impedance ground, and separate clean and dirty wiring zones.
Insertion loss shows how much attenuation the filter provides across a frequency range under specific source and load impedances, usually 50 ohms. Real-world impedances differ, so treat the curves as a comparative guide rather than an absolute promise. Look for filters with high insertion loss in the frequency bands where your device actually emits noise, not just the highest overall numbers.
Medical equipment must meet stricter leakage current limits to protect patients, so filters use smaller Y capacitors or specialized designs, which can limit common-mode attenuation. Industrial environments often have higher voltage transients and motor-driven loads, so filters need larger chokes, higher voltage ratings, and more robust input protection. Choosing a filter rated for the wrong environment can fail safety approvals even if it technically suppresses noise.
Compare the full datasheet parameters, not just the rated current and voltage. Check the leakage current, operating temperature range, insulation resistance, and whether the filter maintains its attenuation under realistic load conditions. Also verify the mechanical mounting and terminal style match your enclosure. A professional filter may have lower losses, better thermal behavior, and documented performance over a wider frequency span, which matters when your product faces compliance testing or field reliability demands.
Conclusion
Getting a product through EMC compliance is rarely about the biggest component on the board. It often comes down to how well the filter at the power inlet or signal line handles the messy, unpredictable noise that real installations throw at it. A filter that looks fine on a spectrum analyzer can fail the moment a nearby motor drive starts switching or a long cable picks up a common-mode transient. That's why the choice between a generic LC network and a purpose-built EMC filter isn't a cost decision—it's a survival decision. Skimping here doesn't just risk a failed test; it leads to field returns, erratic resets, and degraded analog accuracy. The hidden expense shows up in troubleshooting hours and customer dissatisfaction long after the BOM savings have been spent. Matching the filter topology to the actual signal integrity goals matters just as much as the attenuation numbers. A high-speed differential pair needs careful attention to differential-mode filtering without adding too much capacitance, while a low-frequency sensor line may tolerate a stiffer common-mode choke. Getting topology wrong can fix one emission at the cost of introducing signal distortion or ground bounce.
Thermal and layout pitfalls often erase the performance promised on a datasheet. A filter rated for 10 A at 25°C may cook itself when mounted next to a hot switching regulator, because core losses and DCR rise with temperature—and that derating is rarely front and center in marketing material. Return current paths, via placement, and stray coupling between input and output traces can turn a well-designed filter into an antenna if you're not careful about the physical implementation. Testing beyond the datasheet means probing with real-world waveforms: fast edges, burst transients, and impedance mismatches from long cables. The lab setup with a clean 50-ohm source doesn't reflect what happens in a factory with VFDs and arcing contacts. Finally, designing for compliance without over-engineering the BOM is about using the right filter architecture—not stacking three extra stages out of fear. A single well-placed common-mode choke with a carefully chosen Y-capacitor can often beat a brute-force multi-stage filter that costs more and eats board space. The goal is repeatable pass margins, not gold-plated overkill.
Contact Us
Contact Person: Eric
Email: [email protected]
Tel/WhatsApp: 8618117837140
Website: https://www.emcdorexs.com