Professional Insulated Clean Panel Production Line Guide and Best Practices
2026-08-14
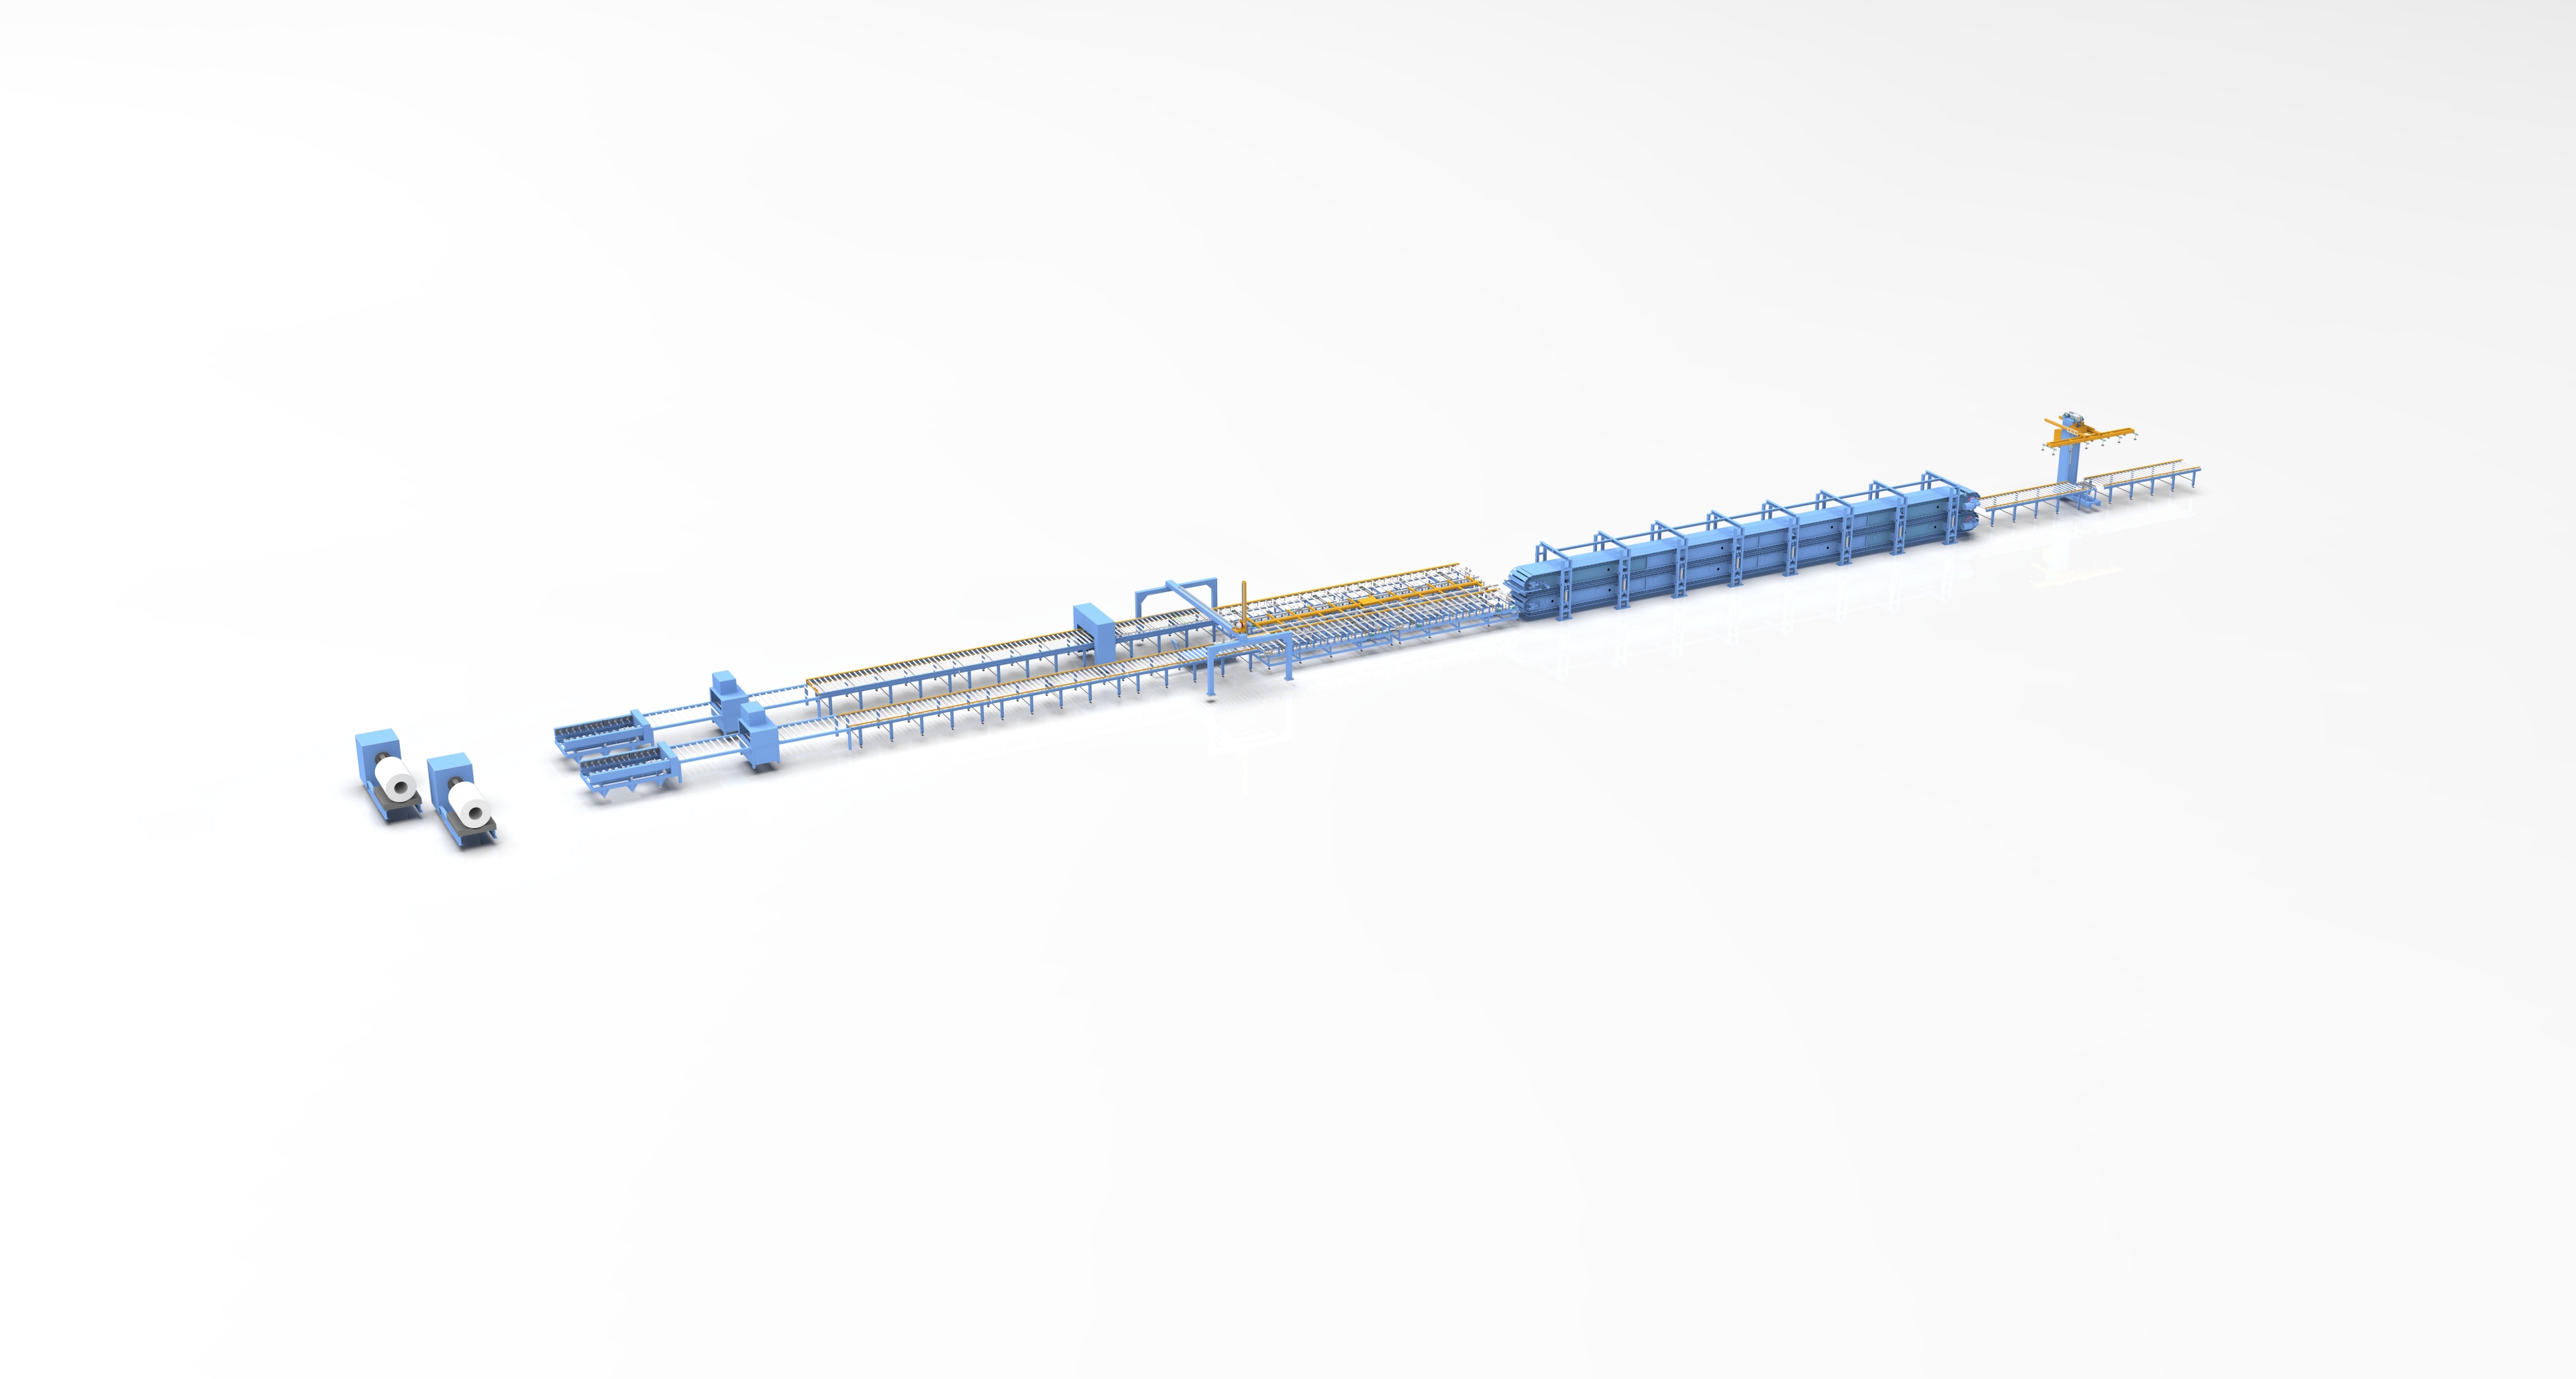
In today's competitive manufacturing landscape, producing insulated clean panels that meet stringent hygiene and thermal standards is no longer a matter of guesswork—it’s a science. Whether you’re upgrading an existing facility or building a new production line from scratch, understanding the nuances of panel lamination, core filling, and edge sealing can make or break your output quality. This guide draws on real-world insights and proven practices to help you avoid common pitfalls and achieve consistent, high-performance results. At the heart of many successful operations is YI ZHOU TECHNOLOGY, whose advanced equipment solutions have redefined efficiency and precision in clean panel manufacturing. Read on to discover the critical factors that separate average lines from truly professional ones—and how to apply them in your own workshop.
Choosing Core Materials That Won't Warp or Delaminate
When you're picking a core, don't get distracted by the face veneers or the fancy finish. Warp and delamination almost always start from the middle. Solid wood can work, but only if it's quarter-sawn, properly dried, and both sides are finished the same way — anything less and it'll cup on you within a season. For anything wider than a cabinet door, I'd skip solid stock altogether and go straight to a high-quality plywood or composite core.
Baltic birch plywood is the default choice for good reason. The thin, void-free plies and cross-laminated construction keep internal stresses balanced, and the phenolic glue lines shrug off moisture far better than standard interior plywood. Marine-grade plywood is another solid option if you can find a truly certified sheet — not the "marine" label some big-box stores slap on. MDF stays flat but turns to mush at the edges once water creeps in, so it only makes sense for dry, fully sealed applications. For high-humidity or outdoor projects, look at compact phenolic panels or bamboo-ply cores; they cost more, but they won't surprise you later.
Delamination is rarely the material's fault — it's usually a weak glue line or trapped moisture. Before committing, inspect the sheet edges for tiny voids or hairline cracks, and match the core's expansion rate to the face material. Better yet, cut a small sample, soak it in water overnight, then bake it in the sun for a day. If the edges stay tight and flat, you've got a core you can trust. Data sheets are nice, but a torture test tells you what actually happens in the real world.
Dialing in Foam Density Without Overcuring the Edges
Getting the density right in a molded foam part often comes down to how the edges behave during cure. The center of the mold holds heat longer, letting the foam rise and stabilize, while the edges lose heat quickly and can lock in a denser, overcured skin. Many people try to fix this by simply adding more blowing agent, but that only makes the middle over-expand and leaves the edges even harder. The real adjustment is in the cure profile, not just the chemistry.
A better approach is to shift heat input away from the mold walls during the first few minutes. Using a lower initial mold temperature or adding a thin insulating liner around the perimeter can slow the edge cure enough to match the center. At the same time, keep an eye on the gel time. If the foam sets too fast at the edges, the blowing agent can't do its job there. A slight reduction in tin catalyst or a switch to a more delayed catalyst can widen the window where density evens out.
Small-batch trials help a lot here. Cast a few parts with the same total mix weight but vary the mold wall temperature by five to ten degrees and watch the density gradient from center to edge. You'll usually find a narrow band where the edge stays soft enough to avoid overcuring while the overall density stays on target. Once that band is mapped, lock the parameters and keep the mold clean, because residue buildup can change heat transfer and throw the balance off again.
What Actually Happens When Line Speed Outpaces Cooling
The first sign is usually dimensional drift. As the line speeds up, the cooling section simply doesn't have enough contact time to pull heat out of the material at the same rate it's being fed. The surface may look set, but the core is still soft. That mismatch means the product leaves the cooling zone with a temperature gradient that keeps shifting after it's been cut or coiled.
You also start seeing surface defects that don't show up at lower speeds. Micro-tears, ripples, or a dull haze appear because the outer skin is freezing too fast while the inside is still expanding. In extrusion or coating lines, this often turns into edge curl or waviness that no downstream tension control can fully flatten. Operators sometimes mistake it for a material problem, but it's really just heat removal lagging behind throughput.
The hidden cost is residual stress. A product that looks fine off the line can warp days later, or fail a drop test because the rapid chilling locked in uneven shrinkage. If the line speed stays too high, those stresses accumulate batch after batch until the rejection rate climbs sharply. Bringing the speed back down isn't just a safety measure; it's often the only way to stop the reject spiral without changing the cooling setup.
Why Panel Flatness Checks Beat Rework Later
Checking panel flatness before installation is not just a box-ticking step—it’s the moment you catch the subtle bow or twist that will haunt the assembly line later. Run a straightedge across the surface and watch for light gaps at the edges; a feeler gauge will tell you exactly how far out of tolerance the sheet has wandered. When you flag a warped panel at the receiving dock, you can reject it, shim it, or set it aside for a less critical cut. That choice takes minutes and costs nothing compared to forcing the piece into place and hoping the fasteners hold.
Rework after assembly is where flatness problems get expensive. Once a distorted panel is bolted or welded to its neighbors, the stresses transfer into the whole structure. You might end up grinding down high spots, replacing stripped fasteners, or cutting out entire sections because one panel refused to lay flat. Every hour spent undoing work is an hour not spent moving forward, and the original material is often scrap by then. A quick check with a laser level or a simple set of winding sticks can prevent that kind of waste.
Building flatness verification into the workflow also changes how teams think about quality. Instead of treating the panel as a finished product that someone else will fix, installers learn to read the surface before touching a tool. Over time, they spot the signs of internal stress or poor storage conditions before the panel ever leaves the cart. That kind of awareness doesn’t come from a manual—it comes from making the check routine, not optional.
Simple Daily Maintenance That Prevents Costly Downtime
Checking a handful of components before each shift takes less than ten minutes, yet it catches the small issues that later turn into week-long outages. Frayed cables, loose terminal blocks, and clogged air filters rarely announce themselves loudly. A quick visual scan plus a temperature reading on critical motors or power supplies gives you enough warning to swap a part during a planned pause instead of after a midnight failure.
The most overlooked daily task is tightening and cleaning. Vibration from normal operation loosens bolts on conveyor drives, pump mounts, and panel hinges. Dust buildup on heat sinks and fan grilles pushes electronics past their thermal limits without tripping an alarm until it's too late. Five minutes with a torque wrench and a can of compressed air prevents the kind of cascade failure that starts with a hot I/O module and ends with a burned-out PLC.
Logging what you find matters more than the fix itself. A simple notebook entry noting "slight bearing whine on conveyor 3" lets the next shift listen for changes. Replace consumables—belts, filters, batteries—on a schedule tied to runtime hours, not calendar guesses. This routine feels mundane, but it turns downtime from an unpredictable emergency into a rare, manageable exception.
When Automation Beats Manual Stacking
There comes a point in any high-volume operation where the steady rhythm of a human hand simply cannot keep pace with the relentless demand for stacked pallets. Manual stacking, for all its adaptability, starts to buckle under the weight of repetitive motion injuries, inconsistent layer patterns, and the creeping fatigue that shows up in the final hour of a shift. Automation steps in not as a flashy upgrade, but as a quiet workhorse that never needs a break, never misjudges a corner, and never lets a half-filled pallet wobble toward the loading dock.
The real tipping point often hides in the numbers that don't make it onto a productivity dashboard. When product dimensions vary slightly from batch to batch, or when a facility runs multiple SKUs through the same line, manual stacking forces workers to make micro-decisions hundreds of times per hour—each one a small gamble on stability and space efficiency. An automated palletizing cell thrives in this environment because it treats every box as a known variable, calculating the tightest interlocking pattern in milliseconds. The result isn't just faster throughput; it's a pallet that survives a bumpy truck ride without collapsing, which is where the true cost of manual error usually surfaces.
There's also a threshold where safety stops being a training topic and becomes an operational liability. Stacking heavy or awkward items at chest height, twisting to reach the far corner of a pallet, and repeating that motion for eight hours—this is where automation quietly outperforms even the most diligent crew. It eliminates the low-grade strain that accumulates into lost-time injuries, and it frees people for tasks that actually benefit from human judgment: inspecting incoming product, adjusting line speed, or spotting a warped board before it becomes a jam. That shift in labor isn't a loss; it's a reallocation toward the kind of work that keeps a facility running smoothly long after the robotic arm has finished its ten-thousandth layer.
FAQ
It depends on the cleanroom class and chemical exposure. For ISO 5 and above, aluminum honeycomb or rock wool with a sealed edge often beats standard PU foam because outgassing and particle shedding are lower. But if budget is tight and the room is dry, high-density PU with continuous metal-faced lamination still performs well—just make sure the edges are fully sealed to stop moisture ingress.
Don't trust the mixing head alone. Calibrate the metering pumps every shift and verify with a beta gauge or laser thickness sensor at the exit of the laminator. Also, check the pressure rollers for parallel alignment weekly—slight misalignment causes wedge-shaped panels that are easy to miss until installation.
Almost always because the two metal skins cool at different rates after lamination, or the core cures unevenly. Stack panels flat with spacers for the first 48 hours, and keep the warehouse temperature stable. If bowing persists, look at the preheating of the metal coils—uneven preheat is a hidden culprit.
They forget to adjust the side forming rolls and end up crushing the edges or leaving gaps. But the deeper issue is not resetting the temperature profile for the new core density. A 50mm PU panel needs different curing tunnel settings than a 100mm panel. Write a changeover checklist that includes both mechanical and thermal adjustments, not just the mechanical.
Focus on edge sealing and corner finish. Large lines are fast but often skim on manual edge detailing. A small line can offer fully welded corners and custom cutouts that big players avoid. Also, invest in a simple traceability system—customers in pharma and food pay more for batch documentation.
If you make more than 500 panels a day, yes. Manual stacking causes scratches and corner dents that lead to rejection. But don't buy a generic stacker—look for one with vacuum suction cups and soft rollers designed for pre-finished metal surfaces. A bad automatic stacker can do more damage than careful workers.
Conclusion
Getting a clean panel line to run consistently starts long before the laminator. Pick core materials with low moisture uptake and good dimensional stability; otherwise you'll chase warping and delamination no matter how tight the rest of the process is. Foam density needs a narrow window, and the trick is to keep heat just high enough for a uniform cure without baking the edges. When the line runs too fast, panels leave the cooling section carrying residual heat, and that hidden stress shows up later as bowing or adhesive creep. Slowing down a little often costs less than reprocessing a full shift.
Flatness checks at the outfeed are not optional; they catch problems while the line is still producing, not after panels are stacked and wrapped. A quick straightedge check every few minutes beats a pile of rejected boards at the end of the day. Daily maintenance also pays off quietly: cleaning rollers, checking temperature sensors, and greasing guides stop small drifts from becoming expensive breakdowns. When volumes climb, automation in stacking and handling usually beats manual labor, but only if the line already has stable quality. Otherwise you just automate the production of bad panels faster, which no amount of handling speed can fix.
Contact Us
Contact Person: Sophia Jiang
Email: [email protected]
Tel/WhatsApp: +86 17367381818
Website: https://yzwelding.com/